


Gun Drilling for Deep-Hole Machining
Review deep-hole gun drilling as a separate operation within a documented shaft route, with drawing requirements and inspection scope kept distinct.
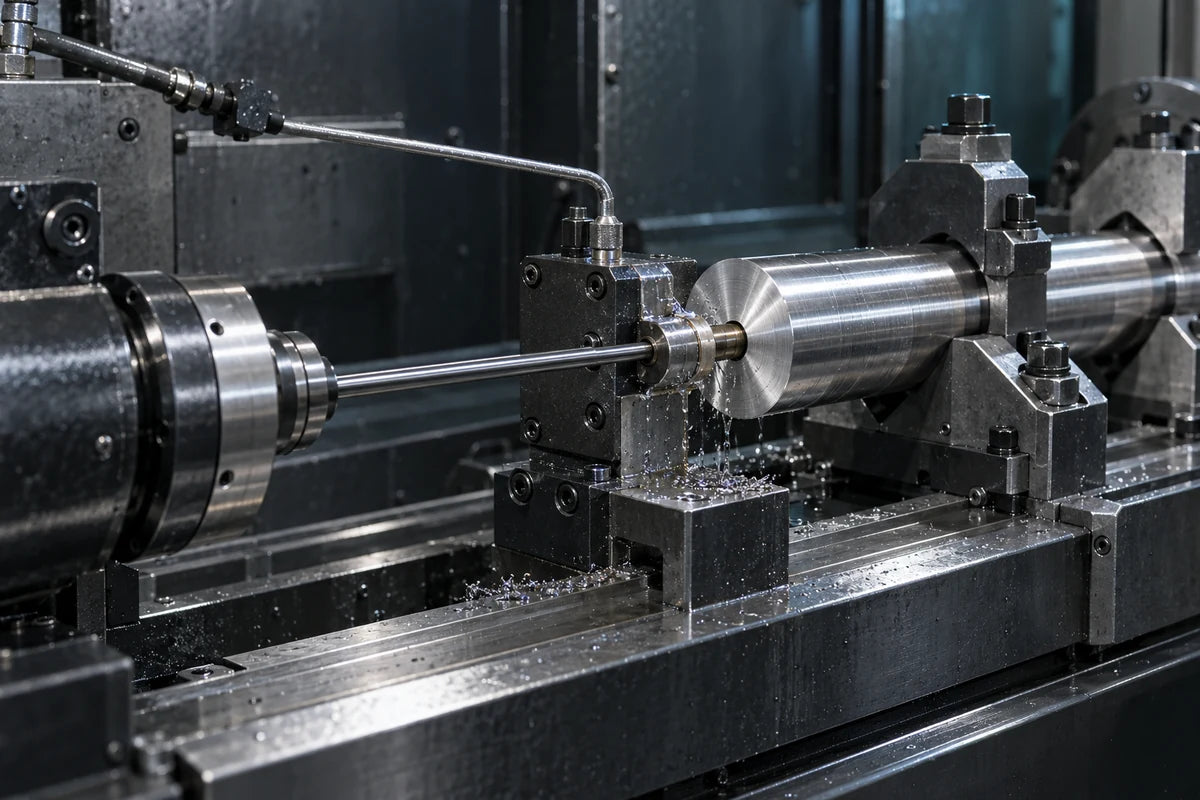
In-house gun-drilling range
Jinhua carries out gun drilling in-house, with bore diameters from 3 to 40 mm and depths up to 500 mm. The applicable diameter-and-depth combination is reviewed against material condition, hole form, entry support and the complete drawing.
Gun drilling within a controlled route
Gun drilling is used for the separate 040 deep-hole operation in the documented automotive steering input shaft route, as confirmed by the Project Owner. Later internal finishing and associated left-end milling belong to the bounded 070 setup; the other end is completed separately in 080.
This is a case-specific process statement, not a general diameter, depth, straightness or tolerance capability commitment.
Keep drilling, datum finishing and inspection distinct
The deep hole and the later datum-related internal finishing have different roles in the process sequence. Do not equate the deep-hole requirement with the drawing datum or treat the whole component as completed in a single setup.
Drawing requirements do not establish achieved bore, positional or phase conformity. The selected dimension records in the case support only their explicitly mapped dimensions.
Is gun drilling the right deep-hole operation for your part?
Review gun drilling as a separate deep-hole operation when the drawing calls for a bore whose depth, entry and access need a dedicated route assessment. Confirm the material and starting condition, the bore function and any later internal finishing before agreeing the operation scope.
Distinguish a drilled intermediate bore from the required finished bore. The documented shaft operation supports its own process story, not a general diameter, depth or straightness commitment for a new enquiry.
What to include in a gun-drilling RFQ
- Provide the controlled drawing revision, material and starting condition, with the required quantity.
- Specify bore diameter and depth requirements, entry geometry and whether the hole is blind or through, including the required end or exit condition.
- Identify intersecting holes, internal features and the functional datum or reference axis.
- Describe subsequent finishing or downstream processing and the bore condition required at handoff.
- State any cutting-fluid, cleanliness or chip-removal restrictions, together with the required inspection, acceptance method and reporting scope.
What shapes the gun-drilling quotation?
The quotation review should consider bore geometry, depth, entry support, guidance and alignment, material condition and any intersecting features. Quantity, required cleaning and inspection reports also affect the scope under review.
Make clear whether the enquiry covers drilling alone or includes a proposed later finishing operation. Compare the same outgoing bore condition and reporting requirements; do not assume the process name includes every subsequent operation.
Define the bore handoff and acceptance records
Confirm the drilling scope, equipment-route suitability and provider responsibility for the actual component. If later internal finishing is outside the enquiry, identify the intermediate bore condition and who is responsible for the subsequent operation.
Agree how the drawing requirements will be checked and which inspection records support acceptance at the specified stage. Inspection access and method suitability need review before commitment; confirmation that gun drilling is used does not establish an achieved bore result.
How guided gun drilling forms a deep hole
Gun drilling uses a long, guided cutting tool to develop a deep bore. Coolant is delivered through the tool, while chips return along an external groove. The tool, guide and workpiece must be aligned for the intended entry.
The operation is planned separately from any later boring, reaming or other internal finishing. These processes may have different functions in the route. The drawing requirement alone does not identify which operation establishes a finished datum or prove the achieved bore condition.
Entry support, alignment and starting condition
Review the bore entry, exit or blind-end condition, material and starting stock before selecting the setup. Guide support near entry and alignment between the tool and workpiece are important planning topics; the actual support arrangement follows the controlled route.
Identify whether the hole intersects another feature and whether later work changes its functional role. Workholding must be considered together with the bore axis and subsequent references. Confirm the equipment and provider arrangement for a new enquiry instead of extending the shaft case into a universal machining range.

Coolant delivery and continuous chip evacuation
A deep bore restricts access to the cutting zone. Coolant delivery and the chip-return path therefore belong in the drilling plan, alongside material behavior and tool condition. Interruptions or poor chip evacuation need assessment for the actual application.
Supply any restrictions on cutting fluid, cleanliness or downstream processing with the enquiry. Entry, exit and intersecting-hole conditions may change the route. This page deliberately gives no universal pressure, diameter, depth or straightness guarantee.
Agree how the bore will be checked
Separate diameter, surface condition, straightness and datum-related requirements where the drawing calls for them. Inspection access becomes a planning issue in a deep bore, so identify the method and reporting scope before treating a requirement as verifiable.
A process confirmation does not supply a missing inspection result. The documented shaft case retains the distinction between the separate drilling operation, later datum-related finishing and selected dimension records. Its unverified bore, position and phase results remain unverified.
Gun-drilling buyer FAQ
Should I request a drilled bore or a fully finished bore?
Specify the bore condition required at delivery and any later operation already planned. Drilling alone and a complete finishing route are different scopes; their responsibilities and acceptance stage must be agreed explicitly.
Why does the enquiry need to distinguish a blind hole from a through hole?
The end condition affects the operation review, chip exit and the required bore handoff. Show the actual geometry and any exit restrictions on the controlled drawing instead of leaving the end condition implicit.
What should I disclose about cross-holes or intersecting features?
Identify their positions and intended condition at the drilling stage, including later operations that create or change them. Intersections need route review for chip evacuation, burrs and the required internal cleanliness.
Can inspection of an intermediate drilled hole replace final-bore acceptance?
Not automatically. If subsequent work changes the bore, agree which requirements apply to the intermediate condition and which records are needed after finishing. The delivery and acceptance stages must refer to the same agreed scope.
What if my deep-bore inspection method is not yet defined?
Identify the drawing requirements and reporting needs in the enquiry and flag the unresolved method. Confirm suitable access and measurement arrangements before committing to acceptance, rather than assuming a standard report covers the bore.
Engineering and quotation questions
Was 040 actually gun drilling?
Yes. The Project Owner confirmed gun drilling for this separate operation in the steering input shaft case.
Does that confirm achieved H8 or positional acceptance?
No. The process confirmation is not an inspection record and does not add a measured acceptance result.
Related CNC process routes
CNC Turning · CNC Milling · CNC Turning-Milling · 4-Axis Machining
Send the drawing for a manufacturing review
Include material, revision, functional datums, starting form, quantity and inspection expectations. Scope and provider responsibilities are agreed for the actual component.
Request a Quote