Prepare a CNC turning enquiry with rotational features, material requirements, datum relationships and inspection questions. Review actual requirements before agreeing a manufacturing scope.
Drawing and datum reviewDefined process routeInspection planning
Workpiece range for shaft-shaped parts
High-volume orders: outside diameters of 5–80 mm and overall lengths up to 350 mm.
Small-batch orders: outside diameters of 5–300 mm and overall lengths up to 800 mm.
The suitable turning route is confirmed from the drawing, material condition, geometry and workholding. These workpiece ranges retain the published feature-specific precision conditions.
How CNC turning creates rotational features
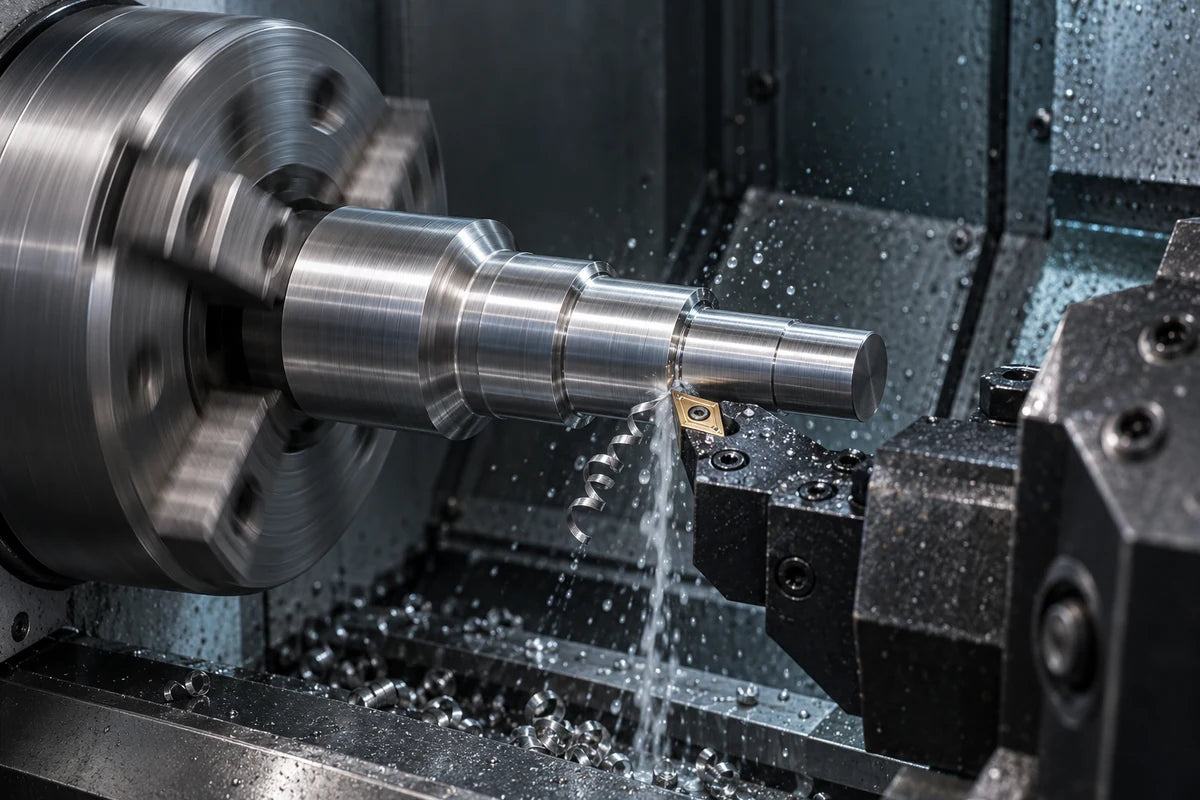
In conventional turning, the workpiece rotates while a single-point cutting tool advances along a programmed path. Longitudinal cutting forms diameters and shoulders; facing establishes end surfaces. Internal turning works inside an existing opening. Roughing removes stock, while finishing addresses the specified size and surface requirement.
A useful drawing review separates the function of each feature: bearing seat, locating bore, shoulder, clearance diameter or end face. The route can then address their relationships rather than treating every diameter as an isolated size.
Workholding, support and datum transfer
Chuck or collet engagement, available grip length and unsupported overhang belong in the setup review. Slender or thin-walled parts need particular attention to support and clamping deformation. Internal boring also depends on tool reach and stiffness.
Identify the radial locating feature and axial stop for each operation. If a component is reversed, explain which finished references are reused and which relationships require checking after transfer. The drawing datum system must not be replaced by whichever surface is easiest to grip.
Chip control and the finishing sequence
Long chips can wrap around a part, obstruct a bore or mark a finished surface. Insert geometry, material, feed, depth of cut and coolant delivery affect chip formation; no single setting suits every workpiece. Internal turning needs a clear path for chips to leave the bore.
For a quotation, identify interrupted cuts, deep bores and surfaces that must remain protected during later operations. Roughing and finishing should be considered with the actual stock condition and workholding sequence, not an assumed universal recipe.
Inspection planned around functional features
Attach the required sizes, form, surface finish and datum relationships to the controlled revision. The inspection plan should identify the characteristic, suitable method, measurement stage and reporting requirement. A size reading alone does not establish positional or runout acceptance.
Where heat treatment or another external process follows machining, clarify which requirements apply before and after that operation and who supplies the corresponding records. Sampling and lot acceptance must be agreed for the order.
Turning process and buying FAQ
When is a second setup needed?
Opposite-end access, grip length and reference relationships can require reversal or another operation. The actual route determines the setup count; turning does not imply one-clamping completion.
What makes an internal bore difficult?
Tool reach, bore access, chip evacuation and workpiece rigidity affect the method. Supply the bore section, depth and functional requirements for review.
How should samples and production quantities be quoted?
State the sample quantity and production batch quantity separately, with expected repeat demand where known. Identify what the sample approval must cover and which requirements also apply to later orders. Ask for the proposed scope and commercial terms for each quantity; this page does not establish a minimum order or lead time.
When should I discuss turning-milling instead of turning alone?
Include flats, cross-holes, slots or other non-rotational features in the complete drawing review. Their relationship to turned locating features may affect the operation sequence and reference transfer. Ask which features belong in each operation; a combined route does not by itself mean that all work is completed in one clamping.
Is CNC turning the right starting point for your part?
CNC turning is a process to discuss when the drawing is organized around rotational features such as an outside diameter, bore or shoulder. A useful quotation starts with the mating function and controlled requirements, not just the overall part shape.
State which features must relate to one another, what starting material is available and where the requested machining scope ends. Flats, cross-holes or other non-rotational features may need a separate operation or a turning-milling route; the actual drawing determines the proposal.
Bearing seats, bores and shoulders: what the drawing must explain
For a bearing seat or another mating diameter, supply the specified fit and mating-part context. Distinguish a locating surface from a clearance diameter; do not replace the drawing requirement with a general request for a “precision part.”
For an internal bore, separate its size from its relationship to the functional outside diameter. For a shoulder, identify the axial location, adjacent mating face and any controlled relationship to the locating feature. Section views help explain bore depth, steps, reliefs and access. These inputs support route review; they do not establish an achieved inspection result.
Choose the enquiry scope around the component
A sleeve or spacer enquiry should identify the bore-to-outside-diameter relationship and the end faces that locate it in assembly. A shaft enquiry may instead centre on journals, axial shoulders and downstream features. For shafts with journals, splines or other functional features, review our drawing-based shaft manufacturing overview.
List the complete feature set even when only part of the manufacturing route is being quoted. This helps separate turning work from later milling, deep-hole work or finishing without implying that those operations share one setup.
Material, blank condition and supplied-stock responsibilities
Specify the exact material designation, condition and starting form. If the enquiry involves a buyer-supplied blank, identify its dimensions, relevant preparation, traceability requirements and who is responsible for supply. Mark unknowns as open questions rather than assuming they are included.
Ask the quotation to distinguish material supply from machining and any subsequent process. Stock suitability and availability require review for the actual part; a material named in an enquiry is not confirmation of inventory or a company-wide processing range.
Quotation inputs for slender, thin-walled or deep-bore parts
For a slender component, show its length, diameters and any restricted support areas. For a thin-walled sleeve, provide the wall section and the surfaces that must remain protected. For a deep bore, show depth, entry access, internal steps and the condition of the starting opening.
Identify surfaces available for gripping and any features that must be completed before or after a reversal. These details let the proposed setup address support, access and clamping effects; they are not a guarantee of a particular fixture, a single setup or an acceptable result for every geometry.
Agree inspection and acceptance before placing the order
Separate the characteristics used for sample approval from those required for production acceptance. Identify the critical fit, bore relationship, shoulder location and surface requirements on the current revision, then agree which checks and reports are included in the quotation.
Specify the required measurement stage, sample or lot identification, reporting scope and any customer acceptance format. A selected size record does not establish every datum relationship, and acceptance of a sample does not automatically establish conformance of a later batch. Required methods and documentation must be agreed for the actual order.
Heat treatment and finishing: define who is responsible
If heat treatment, coating or another operation sits outside the quoted turning work, state who arranges it and which dimensions or surface conditions apply before and after that process. Ask whether the quotation covers pre-process machining, any subsequent finishing work and the corresponding inspection records.
Keep allowance, handling and final acceptance responsibilities explicit in the proposed route. Naming a downstream process is a planning input, not confirmation that Jinhua performs it in-house or supplies that service for every part.
Capability scope and limits
Capabilities are reviewed against the actual drawing, material, functional requirements and inspection expectations.
Individual capability values are documented on the Quality page; they are not reproduced here.
Jinhua uses internal CNC turning and milling where the part geometry and reviewed process route are suitable.
Scope is drawing-specific; it is not a promise for every part, material or operation.
These cases show turning as part of integrated process planning and datum establishment, not general capability or achieved-tolerance promises.
Automotive steering input shaft
Manufacturing challenge
Relate rotational bore and shaft features to left- and other-end work.
Process strategy
Separate deep-hole work precedes the bounded internal-finishing and left-milling setup; other-end completion is separate and retains a unified angular reference.
Why it matters
Shows the connection between internal turning-related references and downstream milling, not a claim that every feature shares one clamping.
Establish rotational features and locating references before different-side machining.
Process strategy
The actual route uses a turning operation followed by two separate 4-axis setups, with documentary locating requirements kept distinct from inspection results.
Why it matters
Explains why turning and datum transfer belong in the complete route rather than an isolated operation list.
Send the current drawing revision, material, quantity, functional datums and inspection expectations. Include starting-form and finishing requirements where known and identify information still open for review.
Does this page establish a tolerance or delivery commitment?
No. Requirements and the proposed route must be reviewed for the actual drawing. Capability scope depends on documented manufacturing and inspection information, and commercial commitments belong in the reviewed quotation.