Plan a CNC milling enquiry around datum faces, hole patterns, slots, pockets, fixture access and inspection requirements. Review actual requirements before agreeing a manufacturing scope.
Drawing and datum reviewDefined process routeInspection planning
Workpiece size for milling enquiries
Jinhua's CNC milling workpiece range is up to 800 mm in length, 500 mm in width and 500 mm in height. The actual part geometry, material condition, clamping surfaces and tool access are reviewed together before agreeing the machining scope.
How milling develops faces, pockets and profiles
Milling uses a rotating multi-edge cutter to remove material as the tool and workpiece move relative to one another. Face and shoulder operations develop reference surfaces; slots, pockets and profiles require a path suited to the geometry and access.
An internal corner is constrained by the selected cutter radius. A deep pocket may need greater tool reach, so geometry, access and rigidity must be reviewed together. Roughing and finishing are different planning tasks rather than one generic pass.
Locate the part before choosing the toolpath
Use the drawing to identify locating faces, secondary references and the features that must remain related. A fixture needs to resist cutting loads while keeping clamps outside the cutter path. Thin sections and irregular cast stock can make support and clamping particularly important.
When another side must be machined, record how the references are transferred. Stock allowance, cast skin and access to the next locating surface belong in this sequence. A stable initial setup does not by itself establish the final datum relationship.
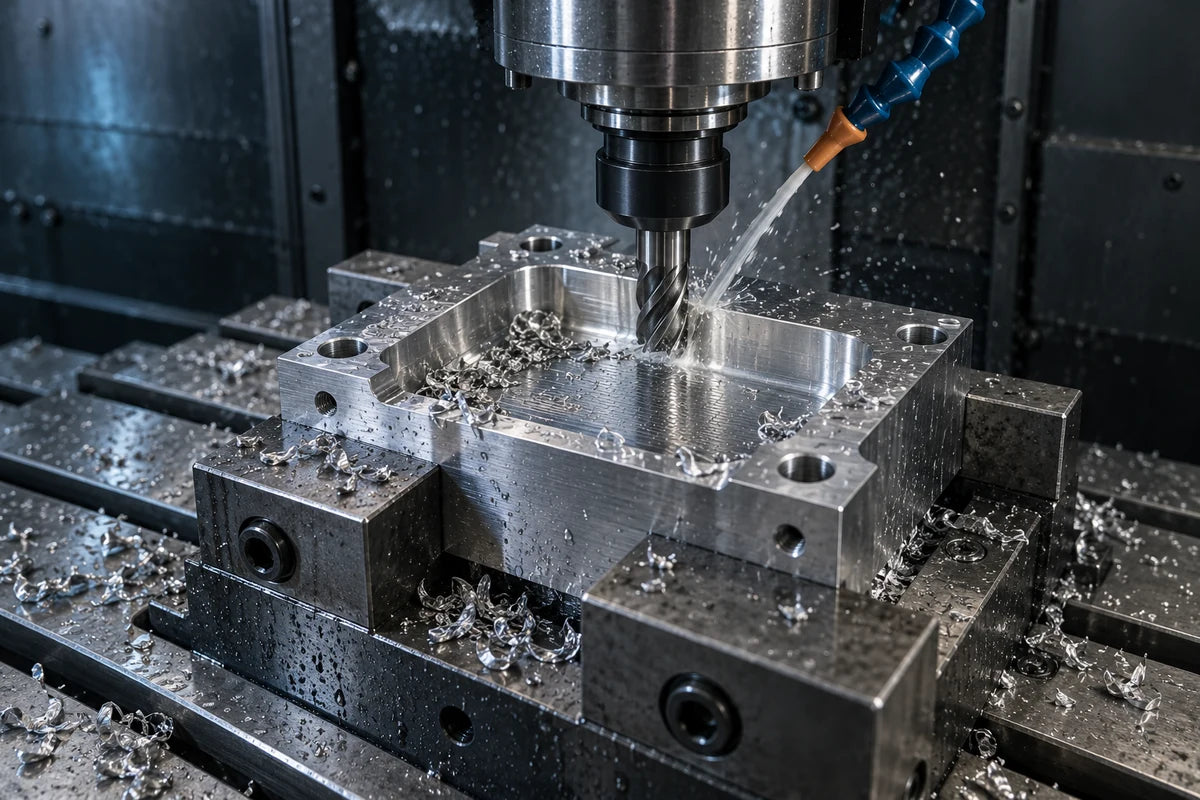
Milling with workholding and coolant.
Pocket access, chip evacuation and cutter engagement
Chips trapped in a pocket can be cut again, affecting the cutting zone and finished surface. Cutter engagement changes at corners and during entry; the path and chip-removal method should account for these changes.
Review material, cutter reach, coolant or air delivery and the geometry of closed spaces. Avoid prescribing universal speeds, feeds or coolant conditions on a service page. The approved route must suit the specific part and equipment.
Check location as well as feature size
An inspection plan for a milled part can address reference faces, pocket dimensions, hole location and specified surface requirements. Identify the datum alignment and reporting method where geometric relationships matter; checking a hole diameter is not the same as checking its position.
Agree which checks happen after each setup and which happen on the finished component. Include burr removal and protection of mating surfaces in the acceptance discussion. Measured results remain tied to the particular part and inspection record.
Milling quotation FAQ
Which pocket corner and depth requirements must the quotation preserve?
Supply section views showing pocket depth, internal corners, floor and wall conditions, and mating constraints. Ask for proposed geometry changes to be identified explicitly. A suggested radius or relief needs approval before the controlled drawing is changed.
What information defines the complete hole and thread pattern?
Show the datum-based pattern, hole function, through or blind condition, thread specification and required depths. Include counterbores, countersinks and intersections with pockets where applicable. Confirm which features and inspection records the quoted milling scope covers.
What should I provide when the blank or clamping access limits milling?
Include available blank geometry alongside the finished drawing. Mark locating and support surfaces, restricted clamp areas, thin sections and faces needing protection. Ask the proposed route to identify its locating sequence and unresolved access questions.
How should burr removal and edge treatment be specified?
Distinguish general burr removal from drawing-controlled chamfers, radii and functional edges. Identify pocket entrances, intersecting holes and mating or sealing boundaries needing attention. Ask which edge work is included and flag any proposed geometry change for approval.
Is CNC milling the right route for your part?
Discuss CNC milling for faces, hole patterns, pockets and profiles that need cutting-tool access around the part. Before requesting a price, identify which features locate or seal the assembly, which remain as-blank and which require machining.
Ask the quotation to define the proposed setup scope, acceptance requirements and unresolved access questions. A proposed route is not confirmation that every drawing requirement can be achieved.
Mark the locating and mating features
Identify the functional datum scheme, mating faces and holes that locate the part in its assembly. Mark which relationships are critical for acceptance and which surfaces only provide clearance. Keep these requirements in the controlled drawing revision rather than relying on an unannotated model.
Separate machined faces from blank surfaces
Show which faces require machining and which may retain the supplied blank condition. Distinguish sealing or seating faces from non-functional surfaces and state where stock must remain for later work. Ask the quotation to identify any unresolved face access or allowance issue before agreeing scope.
Define the complete hole and thread pattern
Identify locating, fastening and clearance holes separately. Show the datum-based pattern, through or blind condition, thread specification and required depths; include counterbores, countersinks and intersecting features where applicable. Ask which hole operations and inspection records the quoted scope includes, rather than treating a list of diameters as the complete requirement.
Show pocket depth and corner constraints
Provide section views for pocket depth, remaining wall and floor conditions, internal corners and restricted tool access. Identify any mating geometry that prevents a radius or relief change. A proposed geometry change belongs in an explicit drawing-review question; it must not be assumed in a quotation.
Clarify relationships across multiple setups
Mark features that must remain related when the component is repositioned. Include faces available for locating and support, restricted clamp areas and surfaces requiring protection. Ask the proposed route to identify reference transfer and access questions. Machining several faces does not, by itself, mean one setup or simultaneous multi-axis cutting.
Send blank and finished-part information together
For a cast or forged blank, include its available drawing or geometry alongside the finished-part revision. Identify proposed machining allowances, blank variation information and who supplies the blank. State the material designation and condition without resolving an uncertain grade by assumption. These are quotation inputs, not a claim about Jinhua's blank-supply model or material inventory.
Specify the inspection deliverable
Mark critical characteristics and explain how they will be accepted: feature size, datum-related location or a mating check may require different records. State whether the enquiry needs selected-characteristic reporting, a specified sample plan or another agreed deliverable. Refer to the existing Quality page for documented context; no measured result is established by this checklist.
Separate quantities, finishing and responsibilities
Distinguish trial-part quantities from expected repeat orders and identify any operation before or after milling that affects a functional surface. State the required finish, blank-supply responsibility and acceptance documents. Ask the quotation to separate included work from customer or external-provider responsibilities; do not assume a batch size, lead time or complementary process is automatically included.
Capability scope and limits
Capabilities are reviewed against the actual drawing, material, functional requirements and inspection expectations.
Individual capability values are documented on the Quality page; they are not reproduced here.
Jinhua uses internal CNC turning and milling where the part geometry and reviewed process route are suitable.
Scope is drawing-specific; it is not a promise for every part, material or operation.
Two casting cases lead this group; the shaft case is a secondary related example. These are drawing-specific stories, not general capability or 4-axis accuracy promises.
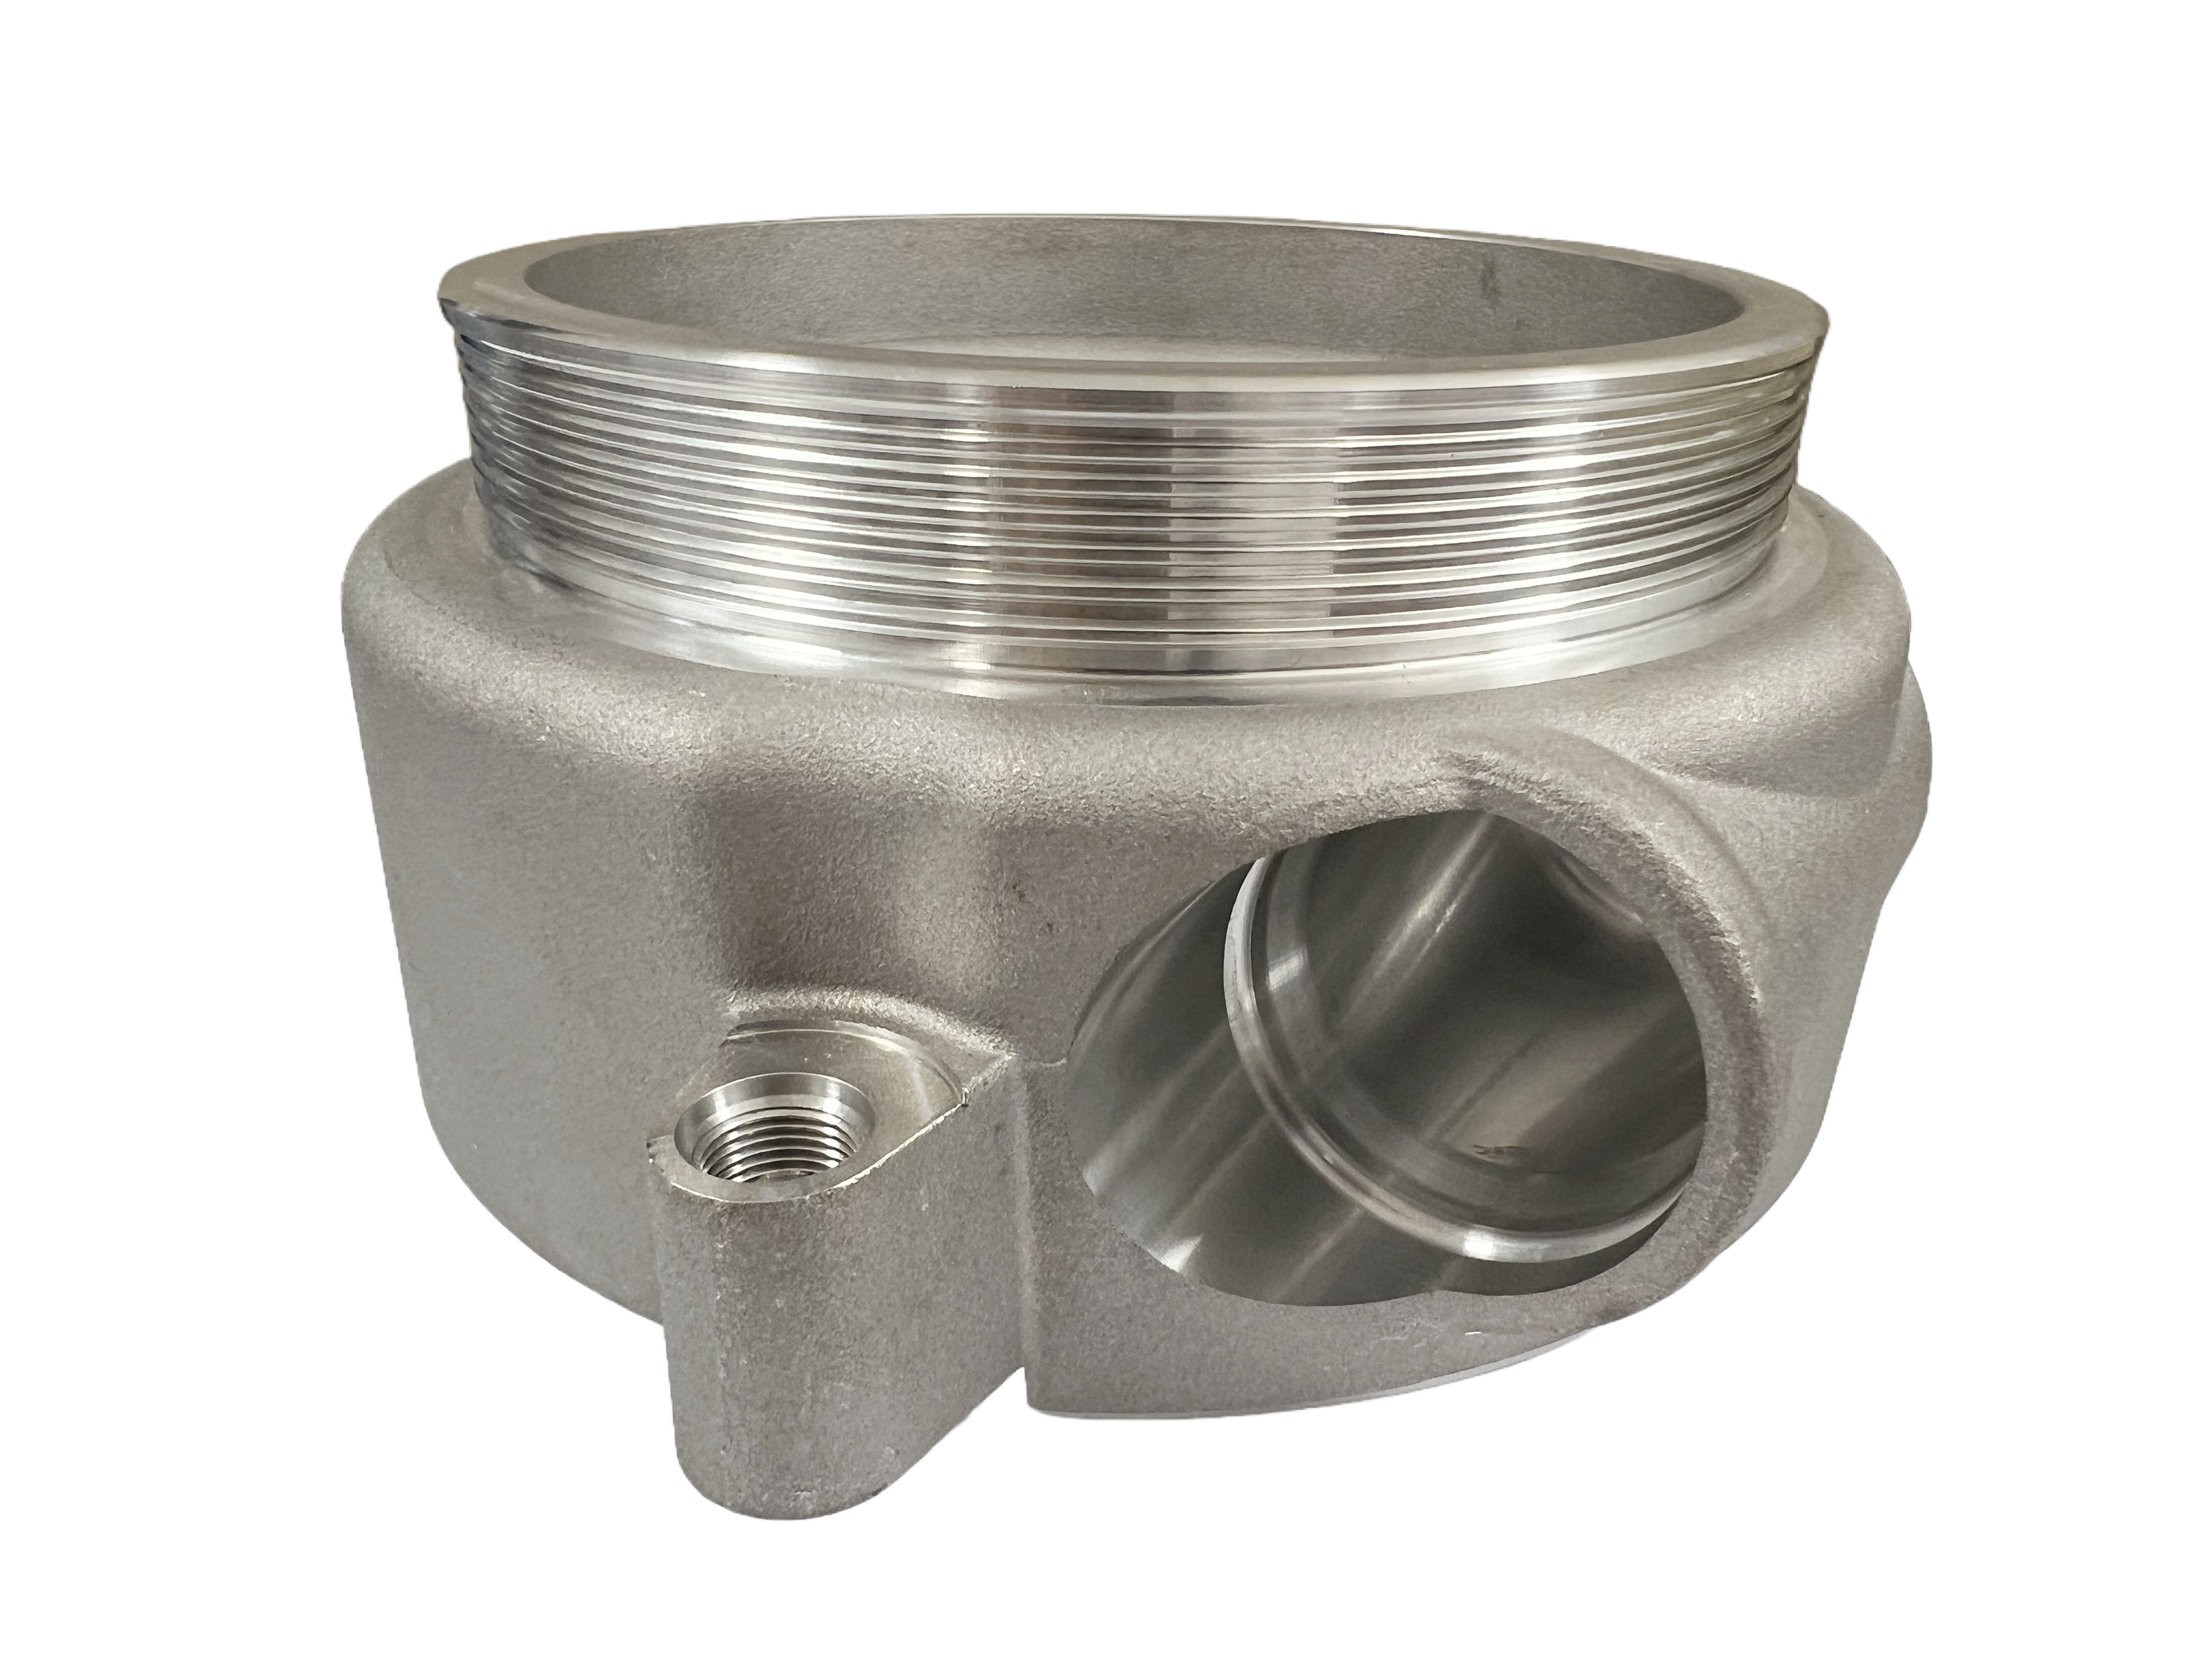
Cast chamber: two 4-axis setups
Manufacturing challenge
Reach side, bore and angular features after the initial turning operation.
Process strategy
Two independent 4-axis setups organize different-side work and transfer locating references; detailed angular features remain requirements, not achieved inspection results.
Why it matters
Illustrates multi-side planning and datum transfer without asserting one-setup completion or quantified accuracy.
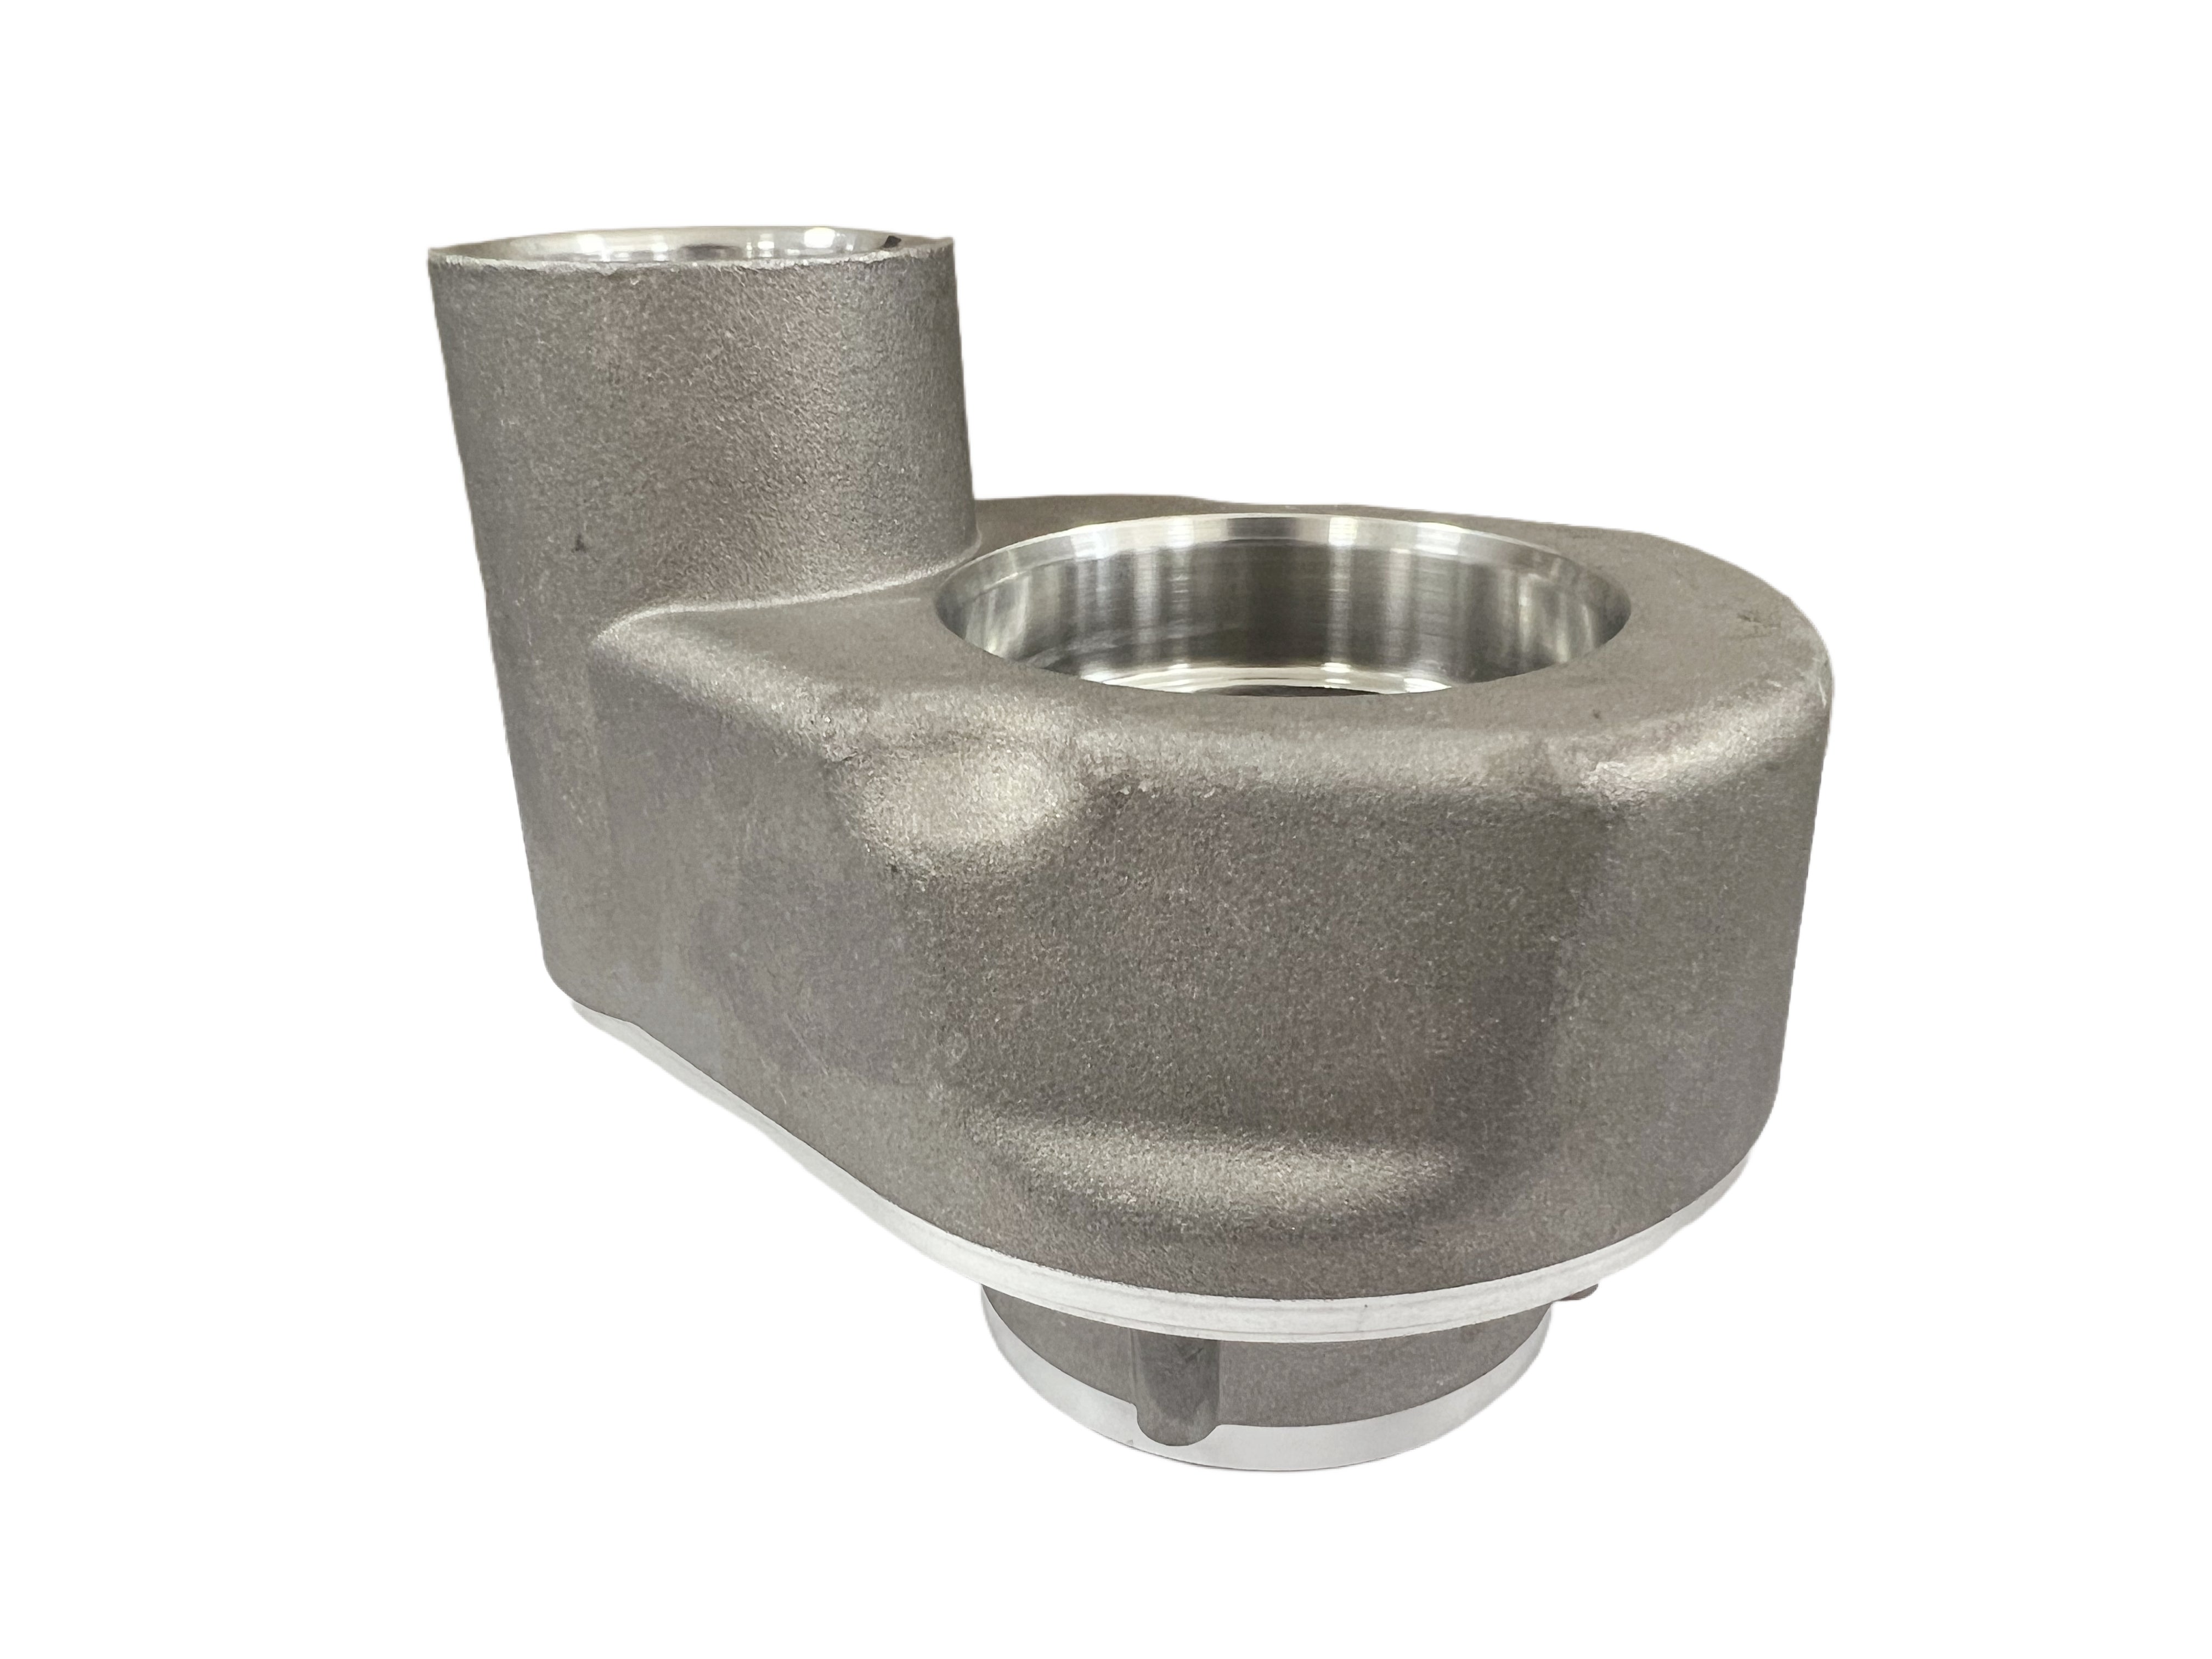
Plan related bores and an angled communicating feature across multiple orientations.
Process strategy
The actual two-setup 4-axis route uses indexing and datum transfer. The communicating-hole detail is a documented process requirement; no measured angular result is claimed.
Why it matters
Shows how bore-system relationships guide milling-led setup planning without introducing a turning process.
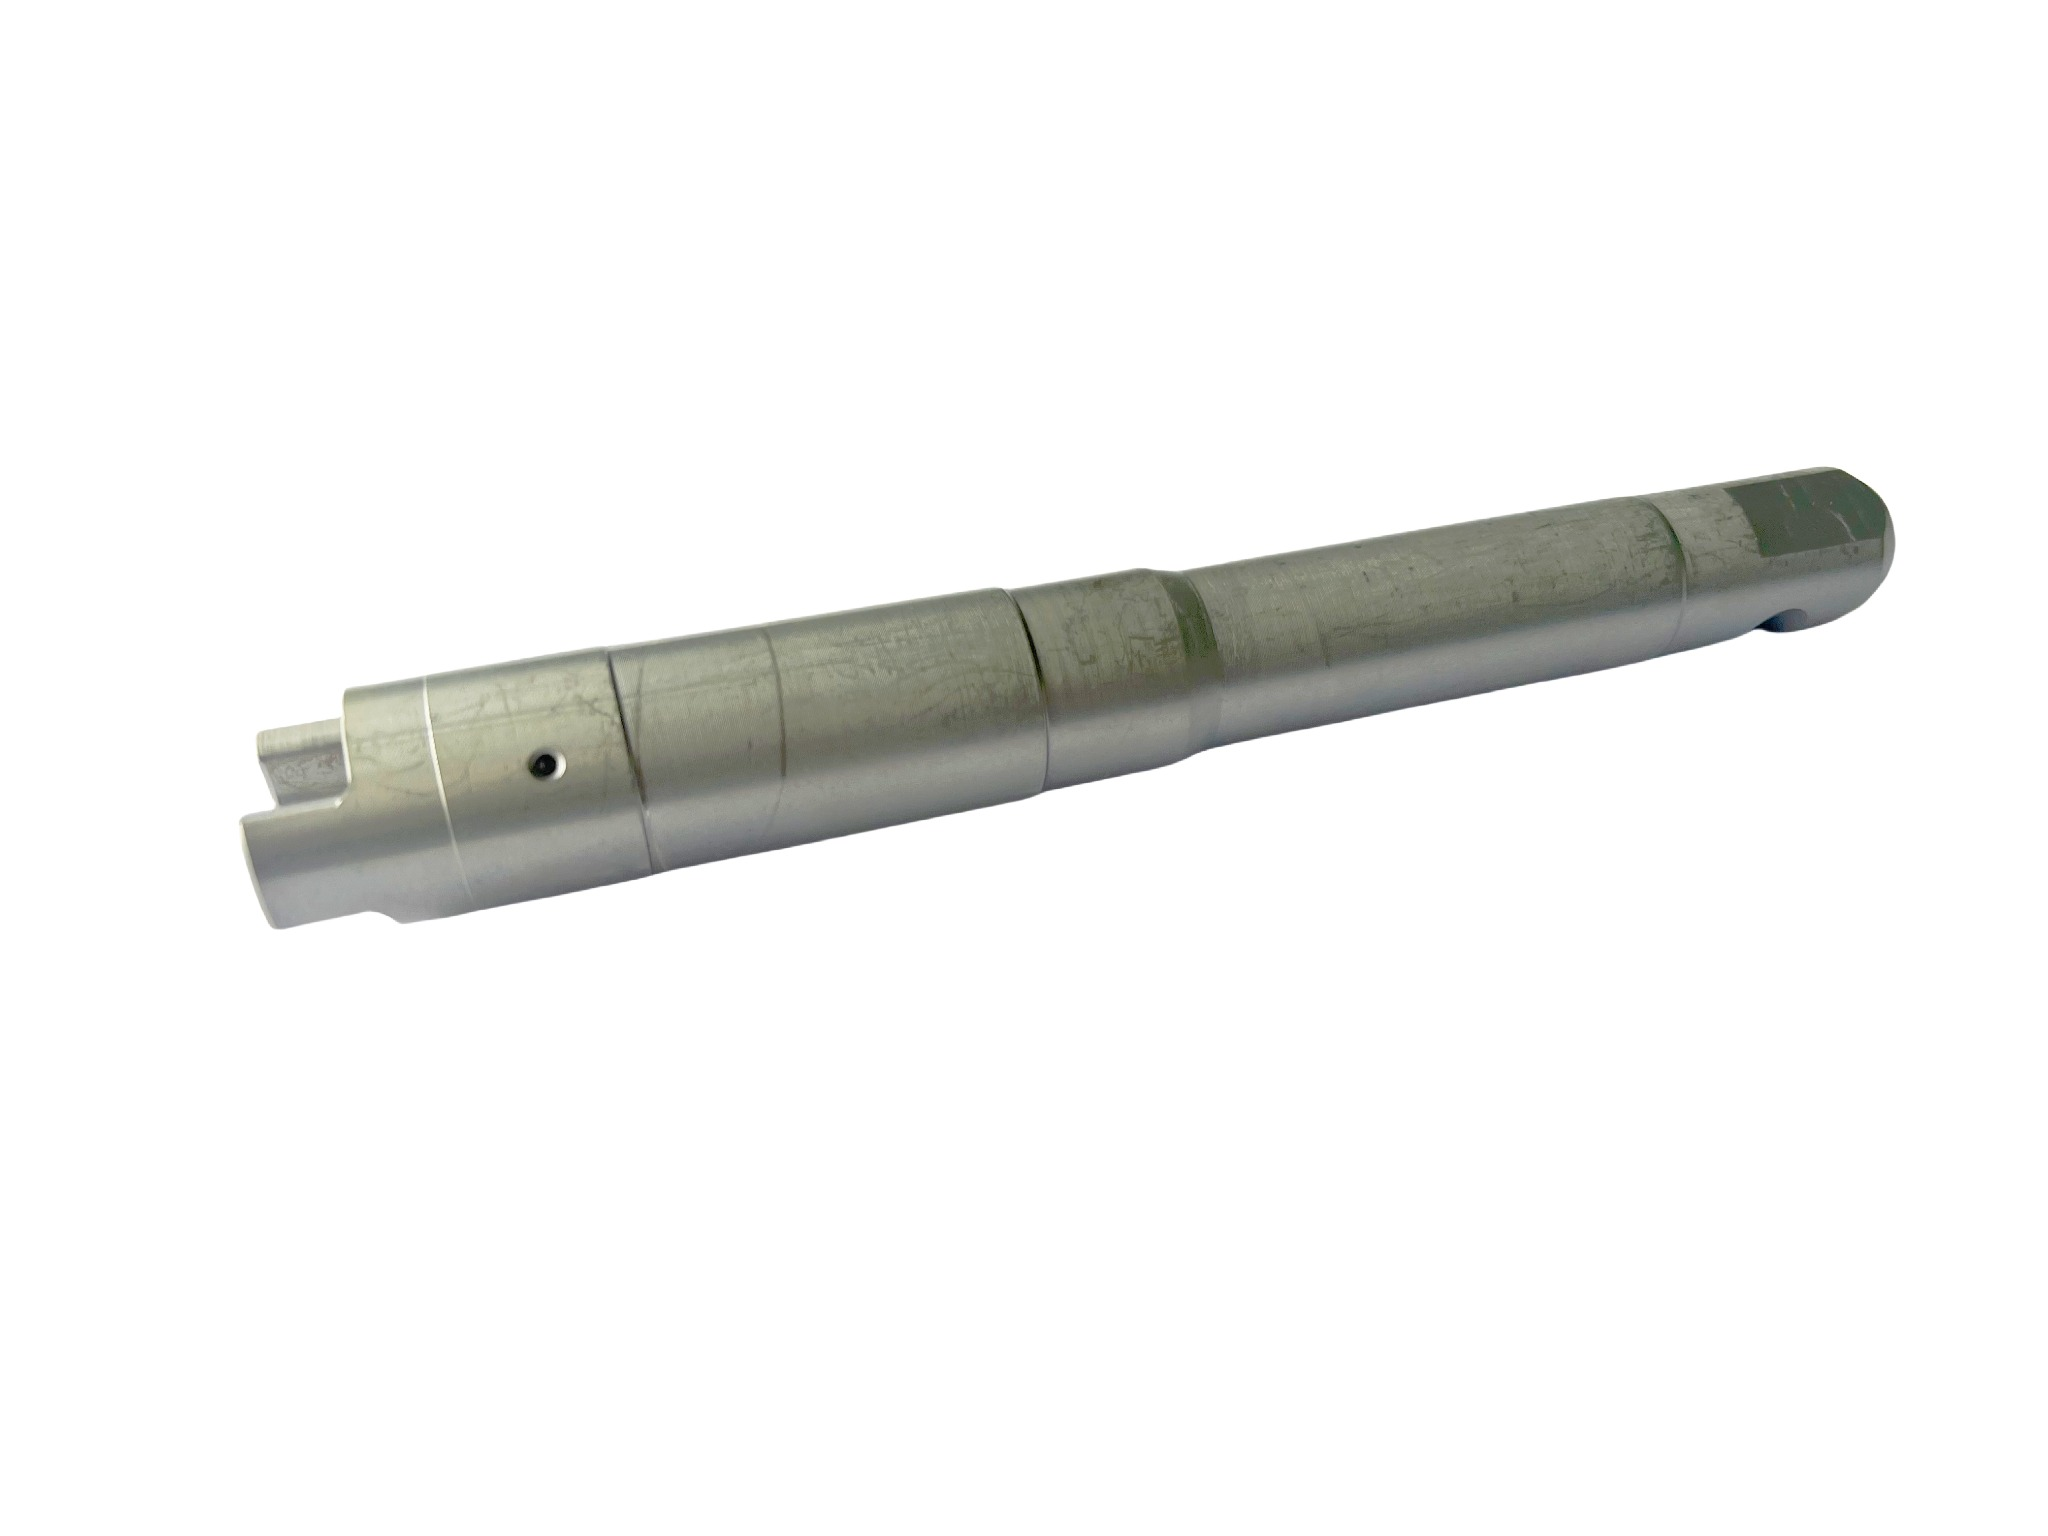
Relate end milling to established internal references and the other end of a shaft.
Process strategy
Bounded shared internal-finishing and left-milling work is followed by separate other-end completion using a unified angular reference; deep-hole work is separate.
Why it matters
Adds a turn-mill reference-transfer example without changing the casting-led focus of this milling page.
Send the current drawing revision, material, quantity, functional datums and inspection expectations. Include starting-form and finishing requirements where known and identify information still open for review.
Does this page establish a tolerance or delivery commitment?
No. Requirements and the proposed route must be reviewed for the actual drawing. Capability scope depends on documented manufacturing and inspection information, and commercial commitments belong in the reviewed quotation.