


CNC Turning-Milling for Drawing-Based Components
Review turned and milled features, datum relationships, setup transfer and inspection requirements with Jinhua drawing-based machining cases.
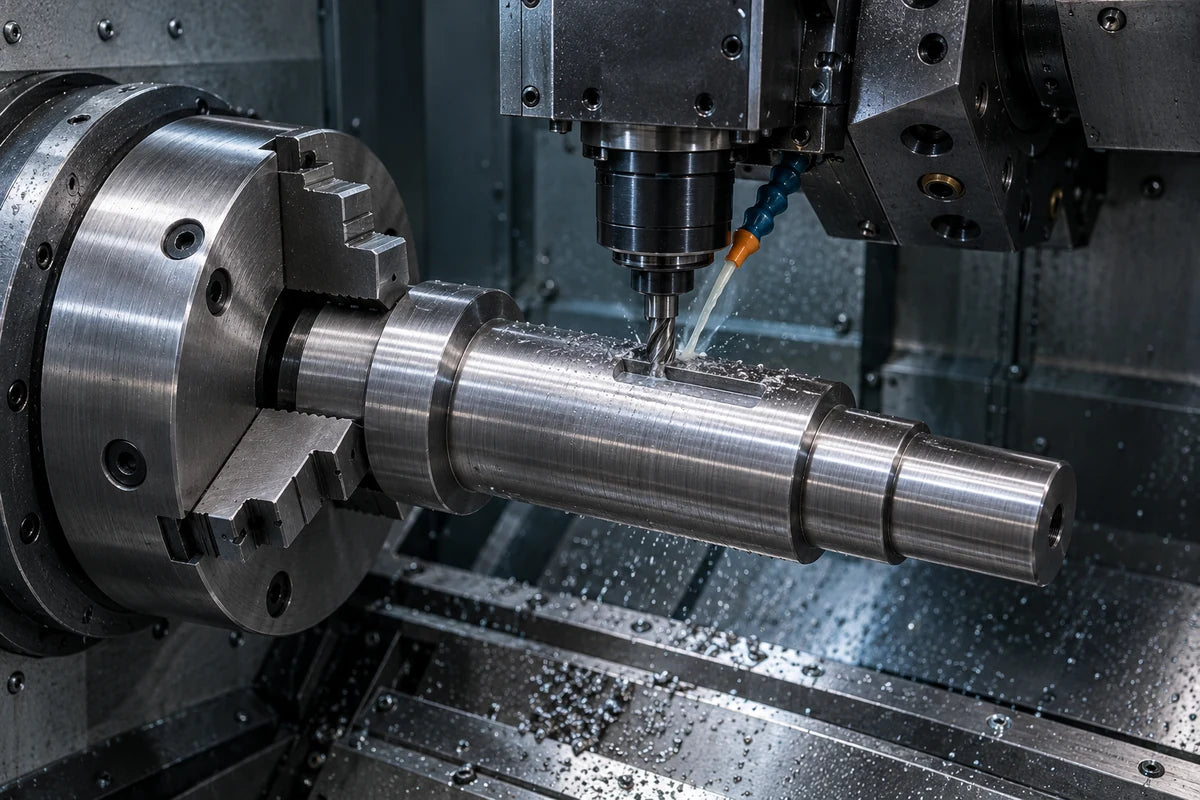
Is a turning-milling route suitable for your component?
Consider a coordinated turning-milling route when a component combines rotational surfaces with milled flats, slots or cross-holes whose relationship matters in the assembly. The drawing review should connect the component axis, axial reference and angular reference to the features that depend on them.
Select the route around those functional relationships, access and setup transfers rather than specifying a machine name alone. A combined route does not by itself establish one-machine or one-clamping completion; the proposed operations need review for the actual part.
What to include in a turning-milling RFQ
- Send the controlled drawing revision, material, starting stock or blank condition and required quantity.
- Identify the turned journals, bores and faces, together with the milled flats, slots and cross-holes that must relate to them.
- Highlight the functional axis, axial datum and angular reference. Identify assembly relationships rather than assuming the clamp surface is the datum.
- State any planned heat treatment, coating or other downstream work, the required delivery condition and which operations are included in the enquiry.
- Specify the inspection and reporting requirements for relationships that cross operation or setup boundaries.
What shapes the turning-milling quotation?
The quotation review should consider feature access, the proposed operation sequence, setup transfers, protection of already-finished surfaces and any downstream work. Quantity and the requested inspection reports also affect the scope being priced.
Compare quotations against the same included operations and final delivery condition. A route that combines turning and milling should not be assumed to reduce cost or remove a setup before the component-specific plan has been reviewed.
Agree the route boundary and acceptance stage
Confirm responsibility for material supply, machining, heat treatment and any external operation before placing the order. If the enquiry covers only part of an existing route, identify the incoming condition, the operations included and the state in which the component is returned.
Agree when acceptance applies and which drawing features, datum relationships and inspection records it covers. Requirements for a new component need their own review; the documented shaft route is not a substitute for those records.
A documented shaft process example
The automotive steering input shaft case records a separate 040 deep-hole operation, a bounded 070 setup for datum-related internal finishing and associated left-end milling, and separate 080 completion at the other end using a unified angular reference. The route keeps these operations distinct.
Read the steering input shaft manufacturing case
The required bore, positional and phase relationships are drawing requirements; they are not additional measured PASS results. Selected inspection records remain limited to the dimensions actually mapped in the case.
Datum and setup review
- Identify the functional bore, journals, faces and angular references on the controlled revision.
- Separate deep-hole drilling from later internal finishing and associated milling.
- Define how references are established and transferred when the component is re-clamped.
- Agree the inspection scope and records for each critical relationship.
Manufacturing responsibility
In the referenced shaft case, machining is distinguished from externally supplied raw material and heat treatment. That case-specific responsibility does not establish the provider route for a new enquiry; confirm it during quotation.
Rotational and non-rotational features in one route
Turning generates rotational surfaces, while milling addresses features such as flats, slots and transverse geometry. A coordinated route plans the connection between those feature families, not merely the order of two process names.
A suitably equipped turning center may use driven tools and controlled spindle orientation for milling. Separate turning and milling machines are another possible route. Neither method is assumed for a new component, and the page does not promise simultaneous machining or universal single-setup completion.
Plan the common references and re-clamping boundaries
Identify the features that establish the component axis, axial location and angular reference. Then assign each critical feature to the operation where it can be reached and located appropriately.
If a part moves between machines or is reversed, the plan should explain how the reference is recovered, how finished surfaces are protected and where transfer-related relationships are checked. A milled flat should not become an angular datum solely because it is convenient for clamping; use the controlled drawing and route.
Different cuts need different chip-control decisions
Turning can generate long chips, while milling produces interrupted cutting and discrete chips. Review each operation separately for material, engagement, coolant delivery and chip exit. Milling near a finished journal also raises surface-protection and burr-control questions.
Clean locating surfaces matter when the part is transferred to the next setup. The route should address trapped chips and burrs at intersecting holes or edges before they affect seating or inspection. The actual method is reviewed for the component rather than inferred from a process image.
Inspect the relationships across operations
The inspection discussion should cover the turned features, the milled features and their specified relationship. Identify which dimensions are ordinary size checks and which require an agreed datum alignment or geometric measurement.
Map each reported result to the feature, part revision and inspection record. A process sequence explains how the component is made; it cannot substitute for a missing positional or angular result. Where material supply, heat treatment or another process is external, retain that responsibility boundary in the route.
Turning-milling buyer FAQ
Do I need to specify one machine in a turning-milling RFQ?
Describe the functional relationships and required delivery state first. If a machine or setup restriction is contractual, identify it explicitly so its suitability can be reviewed rather than assumed from the process name.
How should I identify the relationship between a milled feature and a turned surface?
Refer to the controlled drawing feature and datum system. Identify the flat, slot or hole and the journal, bore or face it must relate to, together with the acceptance requirement for that relationship.
What if heat treatment follows the turning or milling operations?
State the intended sequence and required final condition in the enquiry. Agree the heat-treatment provider, any later machining scope and the stage at which the specified dimensions or relationships are accepted.
Can an enquiry cover only part of an existing turning-milling route?
Propose the specific operations needed and supply the incoming part condition. Feasibility, responsibility for prior work and the outgoing condition must be confirmed before treating the partial route as an agreed order scope.
Which records should be agreed for features spanning more than one operation?
Identify the relevant drawing revision, feature references, datum alignment and reporting requirements. Agree which records support acceptance after the necessary operations, not just checks on an intermediate setup.
Engineering and quotation questions
Is this a single-setup claim?
No. The documented case has separate operations and bounded setup relationships. A new component needs its own reviewed route.
Can inspection targets be treated as achieved results?
No. Drawing requirements and process planning are distinct from the recorded measurements. Only attributable inspection records support achieved-result wording.
Related CNC process routes
Send the drawing for a manufacturing review
Include material, revision, functional datums, starting form, quantity and inspection expectations. Scope and provider responsibilities are agreed for the actual component.
Request a Quote